How to Source Sand Casting Parts in 2026?
How to Source Sand Casting Parts in 2026?
Sourcing Sand Casting Parts in 2026 requires more than comparing supplier prices. It demands evidence of process control, material traceability, delivery stability, and practical engineering support. The global foundry industry remains substantial. Modern Casting’s 58th Census reported approximately 109.6 million metric tons of castings produced worldwide in 2022. That scale reveals strong capacity, but also intense supplier variation.
Details matter.
A reliable sourcing process should examine furnace records, sand-system controls, pattern accuracy, machining allowances, and inspection methods. Request sample dimensional reports, chemical analysis, non-destructive testing records, and corrective-action history. Digital quoting is useful, but it cannot replace a factory audit. I have seen attractive quotations fail after unclear tolerances caused repeated tooling changes and delayed shipments.
John Campbell, a leading casting researcher and author of Complete Casting Handbook, stated, “The casting process is a process of making a shape from a liquid.” His observation remains important in 2026. Liquid metal behavior, mold permeability, feeding design, and cooling conditions determine final quality. A polished supplier website proves little.
Industry forecasts also point toward continued growth in metal casting. Fortune Business Insights estimated the global metal casting market at about USD 151.67 billion in 2023, with further expansion expected through 2032. Forecasts are not guarantees. They may overlook energy costs, regional freight risks, or unstable raw-material pricing.
The strongest sourcing strategy combines technical verification with commercial realism. Check ISO 9001 certification, relevant automotive credentials, capacity evidence, tooling ownership, and communication speed. Ask uncomfortable questions early. A perfect supplier does not exist, and that is worth remembering. The right partner is transparent, measurable, and willing to improve when the first casting is not perfect.
Define Part Needs: Alloy, Weight, Volume, and ISO 8062 CT10–CT13 Tolerance
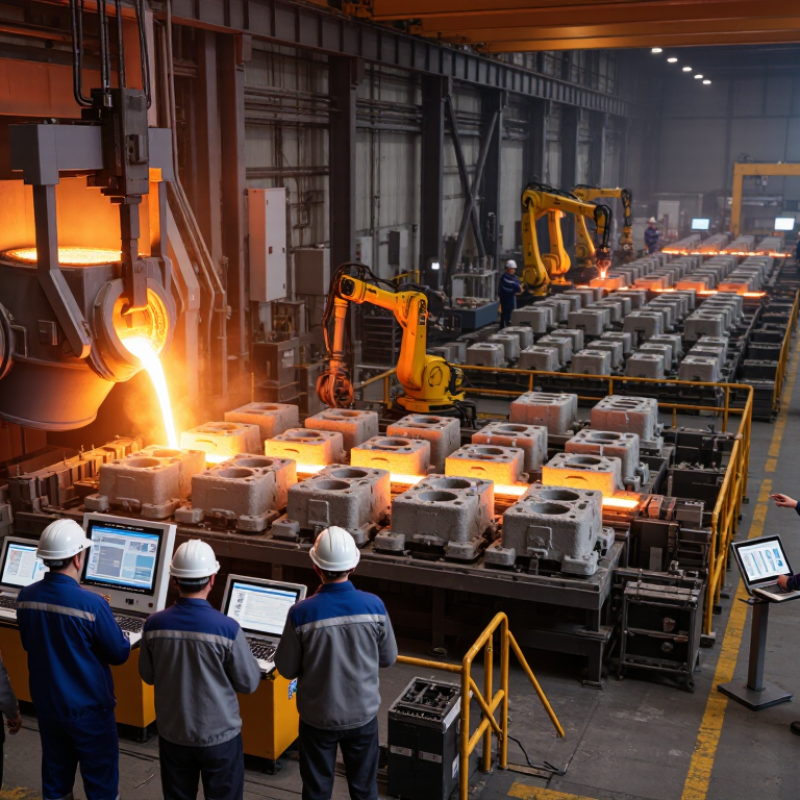
Before requesting sand-cast quotes, define the alloy, finished weight, annual volume, and critical dimensions. A 4-kilogram housing ordered 300 times yearly creates different tooling and inspection needs from a one-off 40-kilogram bracket. State whether weight means the raw casting or machined part. Small details matter. The World Foundry Organization’s 2023 Census of World Casting Production reports approximately 113 million metric tonnes of castings produced globally in 2022. That scale signals a mature industry, but it does not guarantee every foundry suits your alloy or order size.
Specify dimensional tolerance using ISO 8062 CT grades, such as CT10–CT13, against the nominal dimension range. CT10 is tighter than CT13; achievable results still depend on geometry, alloy, mold design, and process control. Identify which faces and holes are functionally critical, and mark them on the drawing. Separate as-cast dimensions from machined features, since machining allowance is not the same as casting tolerance. Ask suppliers to confirm their capability for the actual part, not just quote a grade.
Include alloy designation, target weight, yearly volume, and expected order batches in the inquiry. Request sample inspection results for comparable dimensions, plus the inspection method and measurement points. ISO 8062-3 provides casting dimensional tolerance and machining allowance frameworks; it does not remove the need to agree on drawing requirements. A rushed tolerance choice can look precise on paper. It may still drive unnecessary machining or rejected parts.
Select the Sand Process: Green, No-Bake, or Shell Molding by Volume
How to Source Sand Casting Parts in 2026?
Select the Sand Process: Green, No-Bake, or Shell Molding by Volume
Choosing a sand process starts with annual volume, not a supplier’s sales pitch. Green sand suits repeat production with stable designs and moderate quantities. Its reusable sand lowers tooling expense, but moisture can affect dimensions and surface quality. A production review should check casting weight, wall thickness, alloy, and acceptable finishing work.
No-bake molding fits lower volumes, large castings, and frequent design changes. The process uses chemically bonded sand and usually provides stronger molds than green sand. It can reduce pattern limitations, especially for deep cavities or complex cores. However, binder cost and sand reclamation may raise the part price. Trial castings often reveal issues that drawings miss.
Shell molding becomes attractive when volume and surface requirements justify a more precise pattern. It can produce cleaner details, thinner walls, and more consistent dimensions. Tooling costs are higher, so small orders may not recover the investment. A useful rule is simple: green sand for economical repetition, no-bake for flexibility, and shell molding for refined series production.
A useful rule is simple: green sand for economical repetition, no-bake for flexibility, and shell molding for refined series production.
Real sourcing decisions are rarely perfect. A buyer might select green sand for 2,000 parts, then discover excessive machining on a narrow sealing face. Another project may choose shell molding too early and carry unnecessary tooling expense. Requesting sample castings, dimensional reports, and process capability data can expose these mistakes before full production. Suppliers should also explain their inspection method, not just quote a unit price.
Compare Total Cost: Tooling, Metal, Machining, Scrap, and Freight
When sourcing sand-cast parts in 2026, compare landed cost per accepted part, not the foundry’s piece price. The World Foundry Organization reported 109.6 million tonnes of castings produced worldwide in 2023, across metals and processes. That scale does not predict your quote, but it shows why alloy, batch size, and process assumptions matter. Request tooling as a separate line item, with ownership, maintenance, and expected tool life stated. Then compare metal charges by alloy grade and quoted weight, including gates and risers. Ask whether the scrap credit is based on actual returns or an assumed recovery rate. Small differences add up.
Machining can erase a low casting price. Specify the finished dimensions, critical tolerances, and surface requirements before comparing bids; otherwise, suppliers may price different work. Check whether inspection, packaging, and rejected-part replacement are included. For freight, compare the same delivery basis and shipment size. UNCTAD’s Review of Maritime Transport 2024 documented sharp container-rate swings during Red Sea disruptions, a reminder that a freight estimate can age quickly. Add a validity period to each quote. A common spreadsheet mistake is dividing total cost by ordered quantity, not accepted quantity. That is easy to miss. Recalculate with realistic scrap, machining, and delivery assumptions, then test how a lower-volume order changes tooling cost per part. These estimates will still be imperfect; record the assumptions so the next quote can be checked against actual results.
How to Source Sand Casting Parts in 2026? - Compare Total Cost: Tooling, Metal, Machining, Scrap, and Freight
Illustrative cost model: estimated USD per accepted part for a 4 kg finished aluminum sand-cast housing. The scenarios represent order quantities of 100, 1,000, and 5,000 parts. Figures are planning estimates, not supplier quotations; actual costs depend on drawing complexity, alloy, tolerances, location, and commercial terms.
Estimated landed cost comparison per accepted part (USD) | Cost dimension | 100 parts | 1,000 parts | 5,000 parts | What the estimate includes |
| Tooling amortization | $40.00 | $4.00 | $0.80 | Assumes $4,000 in pattern and related tooling, divided by order quantity. |
| Metal | $18.00 | $16.00 | $15.00 | Aluminum charge allowance, including normal melt and gating losses; alloy and market prices affect the result. |
| Foundry conversion | $38.00 | $22.00 | $17.00 | Molding, core work where required, pouring, shakeout, and routine casting cleanup. |
| Machining | $28.00 | $18.00 | $14.00 | Estimated machining of functional faces and holes; excludes unusually tight tolerances and special finishing. |
| Scrap and rework allowance | $8.00 | $4.00 | $2.50 | Allowance for rejected or reworked castings after normal process controls; not a guaranteed defect rate. |
| Freight | $12.00 | $5.00 | $3.00 | Estimated consolidated domestic freight per part; packaging, distance, and shipping terms can change this cost. |
| Estimated total per accepted part | $144.00 | $69.00 | $52.30 | Sum of the listed cost dimensions. |
| Estimated order total | $14,400 | $69,000 | $261,500 | Per-part estimate multiplied by order quantity. |
Comparison note: Higher volumes reduce the tooling and freight cost allocated to each part and may improve production efficiency. Before comparing supplier bids, confirm that alloy, casting weight, machining scope, inspection requirements, scrap responsibility, packaging, freight terms, and tooling ownership are defined consistently.
Validate Production: PPAP, AQL 1.0, SPC, and On-Time Delivery Above 95%
In 2026, sourcing sand casting parts requires production evidence, not attractive samples. Ask the foundry for a PPAP package before approving regular shipments. It should include the process flow, control plan, material certificates, dimensional results, and signed change records. For a pump housing, request traceability from heat number to mold, pour date, and inspection report. That detail catches gaps early. Do not accept “similar material” without technical review.
Set AQL 1.0 for critical shipment inspections, while defining critical defects separately. A cosmetic sand mark may be acceptable; a blocked passage is not. Use SPC on wall thickness, bore diameter, and key machining allowances. Operators should record readings at scheduled intervals, not only at final inspection. Control charts reveal drift before parts fail assembly. SPC is not magic. A poorly calibrated gauge can produce confident, useless data.
Measure on-time delivery weekly, targeting performance above 95 percent across several months. Define “on time” in the purchase agreement, including partial shipments and agreed date changes. Review late orders with evidence: furnace downtime, tooling repair, transport delays, and corrective actions. One supplier once met the monthly average while missing urgent releases; the metric needed a sharper definition. That uncomfortable finding improved planning. Keep approval conditional until capability and delivery remain stable.
How to Source Sand Casting Parts in 2026?
Validate production with PPAP, AQL 1.0, SPC, and on-time delivery above 95%.
These are validation targets, not measured supplier results: require PPAP approval before production and aim for on-time delivery above 95%. Define AQL 1.0 in the agreed sampling plan; it is not a guarantee of a 1% defect rate. Use SPC to monitor process stability and respond to out-of-control signals.